
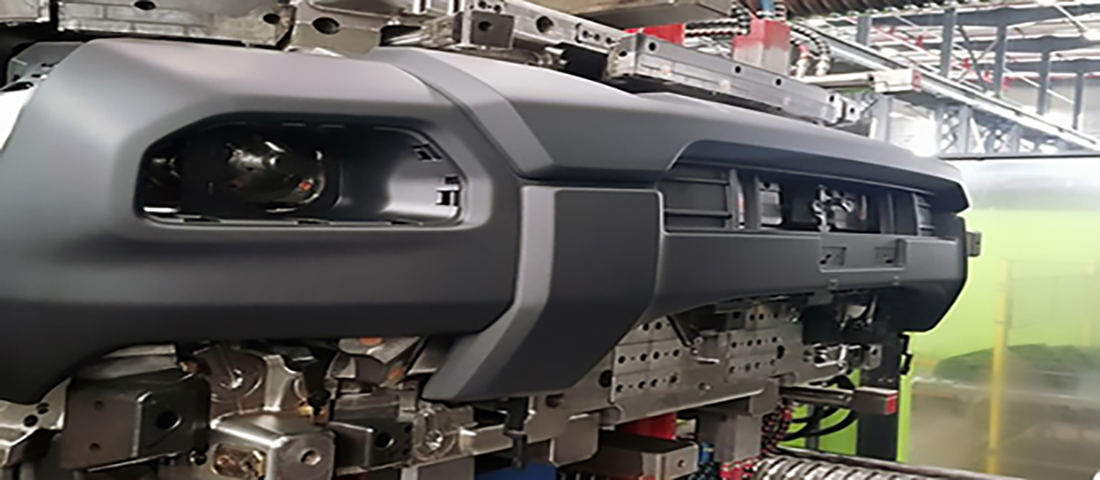
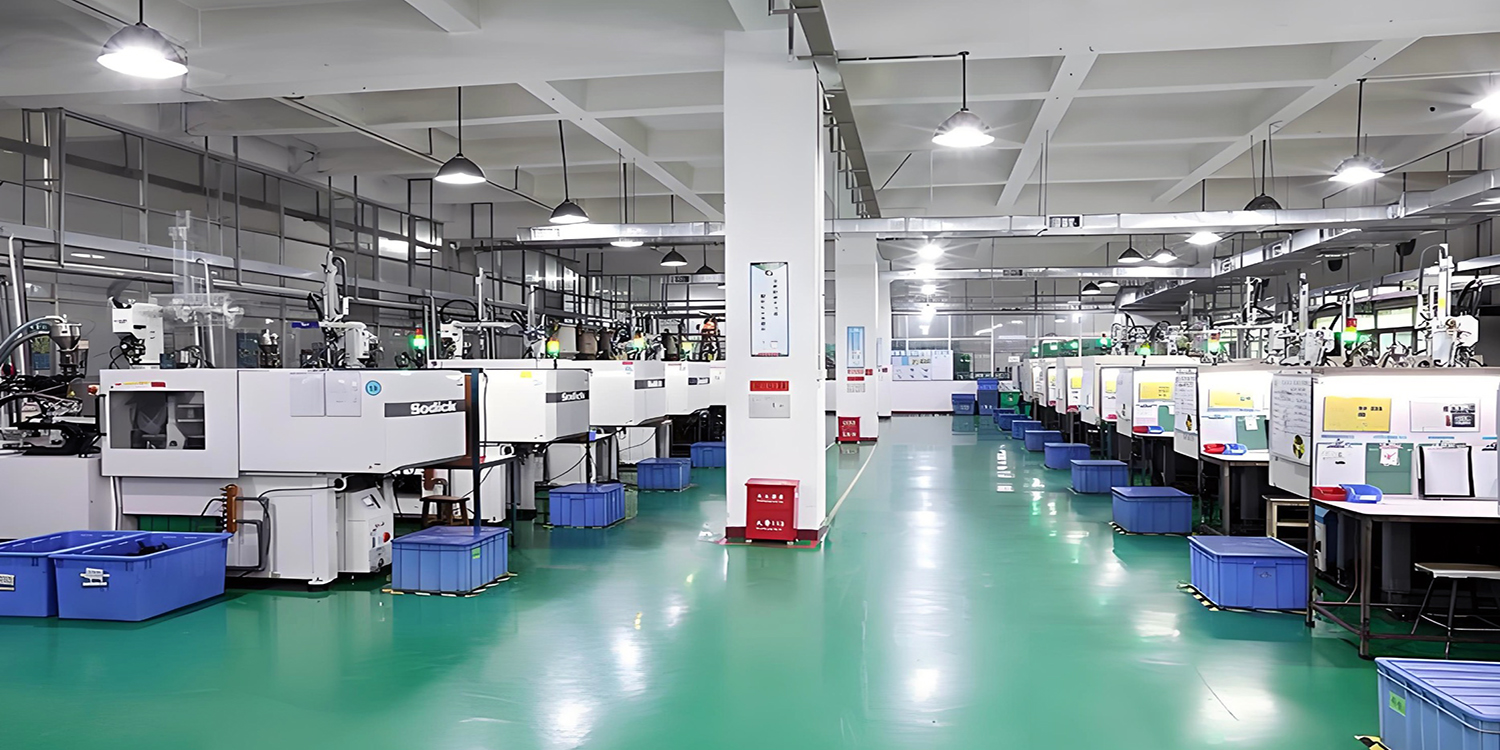
injection molding shop
FMS Molding Team Is Your Trusted Partner for Precision Mold & Injection Molding Since 2009
For nearly two decades, FMS has delivered world-class tooling and turnkey injection molding solutions to a global clientele. We specialize in custom plastic injection molding across highly demanding industries, including Medical, Automotive, Electronics, Packaging, Food & Beverage, and Outdoor Sports/Hunting.
Why Global Brands Choose FMS:
• Advanced Automation & Speed: 100% of our injection molding machines are integrated with high-speed robotics, ensuring consistent high quality, flawless precision, and minimized cycle times.
• High-Capacity 24/5 Operations: Operating on a 3-shift, 5-day schedule (with scalable weekend overtime), our workshop ensures your mass production deadlines are always met, no matter the volume.
• Engineering Excellence: Our veteran mold and design engineers bring deep cross-industry expertise, helping you optimize complex geometries for manufacturability (DFM) and cost efficiency.
• End-to-End Control: From initial tool design and steel/aluminum mold machining to final parts production, every step is managed entirely in-house by the FMS team for strict quality assurance.
Partner with FMS today to transform your complex designs into high-quality, cost-effective realities.
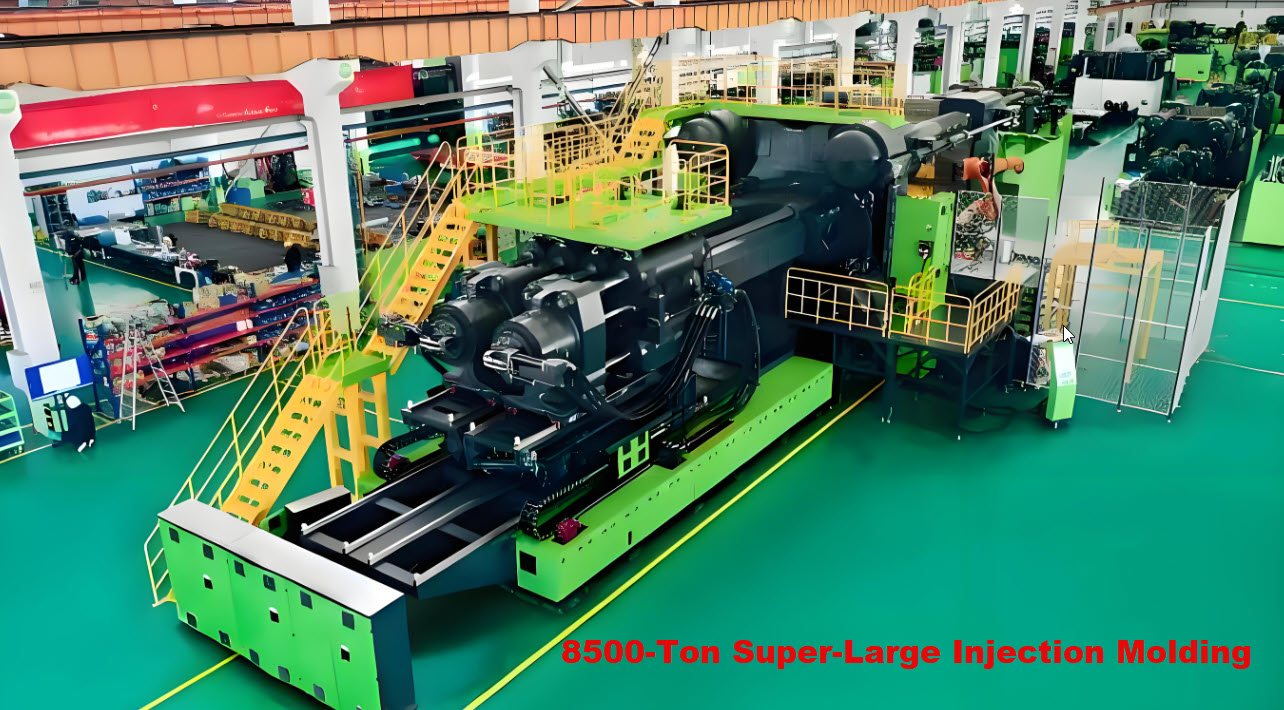
8500-Ton Super-Large Injection Molding Machine
How Does Injection Molding Work?
A special-purpose injection molding machine carries out injection molding. The manufacturing process is divided into the various steps listed below:
Step 1 – Creation of the Mold
The first step in injection molding is mold creation. The mold for the part to be manufactured is designed according to the specifications of the part’s 3D model, using computer-aided design, following several injection molding guidelines. It is then manufactured in two parts, usually using CNC machining. Molds are made from metals (mainly steel or aluminium).
Step 2 – Injection
The separate halves of the mold are placed in and held together tightly by the clamping unit of the injection molding machine. In the form of granules or pellets, the raw material is introduced into a barrel where it is heated at a high temperature and pressure till it melts. Now in molten form, the material is immediately injected into the mold cavity, filling the entire space in the mold. It then cools down and solidifies, forming the shape of the mold.
Step 3 – Ejection and Finishing
After the material has completely cooled and solidified, the mold is opened by the clamping unit and the solidified finished part is ejected. The finished part is subjected to some post-processing operations. These operations include removing excessive material and support structure, surface finishing, and, if required, painting, electroplating, heat treatment, etc.
Other Injection Molding Processes:
Over Molding
Over molding is an injection molding process that allows a part to be created from two different materials. The first material is molded and, before cooling down, the overmolding material is introduced, creating strong bonds between the substrate and the overmolding material. This technique is used to create multi-material objects with improved aesthetics and functionality, while eliminating the need for secondary operations.
Insert Molding
Insert molding is similar to over molding. In this injection molding technique a preformed object is inserted into the mold before the molten material is poured. With the point being to have the preformed material inserted into the molded object. An application of insert molding is inserting metal screw holes into plastic parts.
Metal Injection Molding
In this process, finely powdered metal is combined with wax, polypropylene binders, or other polymers to form a feedstock mix. It is then injected into the mold and left to cool. Once it solidifies, a portion of the blinder is removed using methods such as the catalytic process and the use of solvents.
Die Casting
The die casting process, also known as high-pressure die casting, is the forcing of molten metal under high pressure into a mold cavity. The process is as follows:
First is the preparation of the dies (molds), which entails the lubricating of the mold cavity to facilitate the easy removal of the casting and to control the temperature.
After that, the cast is closed and injected with molten metals under relatively high pressure between 1500 psi and 25400 psi.
Die casting products are made from nonferrous metals such as copper, zinc, aluminium, and lead.
Thin-wall Injection
This injection molding process is used to create plastic parts with very thin walls such as food packaging, parts of equipment, and lab apparatus. The sizes of these parts are larger than their thickness. This process of creating thin walls is more difficult than other processes.
Micro Injection Molding
Just as the name implies, “micro injection molding” is a molding process used to produce tiny plastic parts with weights of about 1 to 0.1 grams. This facilitates the manufacture of micro parts of various complicated geometries with maximum precision and accuracy.
Gas-assisted Injection Molding
In the production of thick plastic parts with injection molding, there’s the risk of distorted parts caused during the cooling process of the molten plastic. This is prevented from happening in gas-assisted injection. As the molten plastics solidifies, gas is introduced into the mold by gas channels, producing smooth surfaces.
The Future of Plastic Injection Molding
The future is bright for the plastic injection molding industry, with several new technologies showing a great degree of promise.
Internet of Things (IoT) technologies like sensors and automation solutions, for instance, allow for increased connectivity across the entire production system. This provides better visibility into the status of the injection molding process while also better positioning manufacturers to produce higher-quality parts at reduced costs. Automated solutions like robotic unloaders that can stack and unstack parts more efficiently can use programmable setups, sensors, and other IoT features to help shorten production timelines without sacrificing part quality.
Micro-injection molding is another emerging process that applies the mechanisms of injection molding at a microscopic scale. This is especially of interest in medical device manufacturing circles, where the technology could allow product teams to design smaller device assemblies capable of performing potentially life-saving procedures using less-invasive methods and tools.
Eco-friendly injection molding materials are increasingly in demand. While most thermoplastics can be reclaimed and reused simply by melting and re-integrating them, sustainability advocates are pushing for more ambitious goals. Out-of-the-box thinking is leading manufacturers to develop and use materials with less or no thermoplastic content, including next-generation, plant-based materials like corn- and flax-based plastics.
The Development and Emergence of Plastic Manufacturing. The history of plastic injection molding begins in 1868 when inventor John W. Hyatt patented the process of creating celluloid, a material originally intended to replace the ivory used in billiard balls. In 1872, Hyatt and his brother Isaiah patented the first injection molding machine, which used a simple plunger mechanism to push celluloid through a heated cylinder and into a mold. The device led to the development of a booming manufacturing industry that produced buttons, combs, collar stays, and other items from celluloid.
Soluble forms of cellulose acetate became available in the early 1900s, offering a much less flammable substitute for previous materials. In the lead-up to World War II, many of the thermoplastics commonly used today — including polystyrene and polyvinyl chloride (PVC) — were developed.
The Impact of World War II on Plastics Manufacturing
Developments in warfare technology, including aircraft, marine battleships, tanks, and other forms of weaponry, consumed vast amounts of raw materials during the course of the Second World War. The post-war industrial boom experienced by many developed Western countries coincided with skyrocketing demand for affordable materials that could be used to mass-produce parts. This was due in large part to how the war disrupted global shipping lanes and required the extraction of huge amounts of natural resources to manufacture tanks, ships, and other war-time products, leading to worldwide shortages of rubber and metal.
Thermoplastics presented affordable options capable of filling many of the market gaps created by these material shortages. Injection molding made it possible for manufacturers to quickly and cost-effectively manufacture parts in large volumes. As markets and supply chains worldwide shifted toward plastic, injection molding emerged as a mainstay and fixture for modern manufacturing companies.
In 1946, James Watson Hendry’s extrusion screw injection machine revolutionized the modern plastic injection molding field. The machine’s rotating screw gave the operator better control over the production process, resulting in significant improvements to the quality of the injection-molded parts. Hendry also pioneered the gas-assisted injection molding process, which made it possible to manufacture long and complex hollow parts.
During the latter half of the twentieth century, plastic materials became more advanced and competitive, offering comparable strength to some metals but at a greatly reduced weight.
Plastic production overtook steel production in terms of market share by the 1970s, and the introduction of lightweight aluminum molds in the 1990s offered a faster, more cost-effective substitute to steel tooling in some instances.
Assuming that the mold has already been created, injection molding becomes an easily-repeatable process consisting of six discrete steps:
1. Clamping
The first step of the injection molding process is clamping. Injection molds are typically made in two, clamshell-style pieces. In the clamping phase, the two metal plates of the mold are pushed up against each other in a machine press..
2. Injection
When the two plates of the mold are clamped together, injection can begin. The plastic, which is typically in the form of granules or pellets, is first melted down into a complete liquid. Then, that liquid is injected into the mold. Manufacturers should take care to ensure the temperature remains constant throughout this step of the process
3. Dwelling
In the dwelling phase, the melted plastic fills the entirety of the mold. Pressure is applied directly to the mold to ensure the liquid fills every cavity and the product comes out identical to the mold.
4. Cooling
The cooling stage is the most straightforward; the mold should be left alone so that the hot plastic inside can cool and solidify into a usable product that can be safely removed from the mold.
5. Mold Opening
Once the part has cooled, a clamping motor will slowly open the two parts of the mold to make for a safe and simple removal of the final product.
6. Ejection
With the mold open, an ejector bar will slowly push the solidified product out of the open mold cavity. The fabricator should then use cutters to eliminate any waste material and perfect the final product for customer use. Waste material can often be recycled and reinjected for the next part, decreasing your material costs.
Injection molding is process tailored for producing large volumes of parts. Compared to other manufacturing technologies—like CNC machining and 3D printing—it requires an upfront, capital investment into tooling. But individual piece-part price will be substantially less when compared to other means of manufacturing plastic parts. This cost structure makes it an affordable solution for production runs.
It’s most often used for the manufacturing plastic parts at scale due to its low material waste and low cost per part. It’s an ideal manufacturing process for industries like medical devices, consumer products, and automotive to name a few.
How Does Injection Molding Work?
Tooling fabrication: Once an injection molding design is finalized the first step in the manufacturing process is to mill the tooling, which is typically fabricated from steel or aluminum. In most cases, the metal block of material is placed in a CNC mill, which then carves out a negative of the final plastic part. Additional treatments like polishing or laser etching can then be applied to the tooling to achieve specific surface finishes.
Part production: The actual production of plastic parts begins by loading resin pellets into a barrel. The temperature of the barrel is raised until the resin pellets reach a molten state and are then compressed. Next, the molten plastic is injected into the metal tool through a runner system, which then feed into the mold cavity through gates. The part then cools down, solidifies, and is ejected from the tool with ejector pins.
Types of Injection Molding
The term injection molding encompasses a handful of processes that inject liquid resin into a tool to form plastic parts. Here are four common types:
Thermoplastic injection molding: Thermoplastic injection molding is the most common type of molding. It injects thermoplastic resin into the mold where the material cools to form the final part.
Liquid silicone rubber molding: Liquid silicone rubber uses thermoset materials and a chemical reaction creates the plastic part.
Overmolding: Overmolding is a process used to manufacturing plastic parts with two or more materials. You’ll often find this on parts to improve grip by adding rubber to the handle.
Insert Molding: Insert molding is process that begins with an insert component placed into the mold before resin enters. The material is then injected and flows around the insert, typically metal, to form the final part. This is frequently used for parts that require metal threads.
Injection molding is a complex manufacturing process. Using a specialized hydraulic or electric machine, the process melts, injects and sets plastic into the shape of a metal mold that’s fitted into the machine.
Plastic injection molding is the most widely used components manufacturing process for a variety of reasons, including:
Flexibility: manufacturers can choose the plastic injection mold design and type of thermoplastic that’s used for each component. This means the injection molding process can produce a variety of components, including parts that are complex and highly detailed.
Efficiency: once the process has been set up and tested, injection molding machines can meet high volume production. Using electric injection molding machines also makes the process relatively energy efficient.
Consistency: if the process parameters are tightly controlled, the injection molding process can produce thousands of plastic parts quickly at a consistent quality.
Cost-effectiveness: once the mold (which is the most expensive element) has been built, the cost of production per component is relatively low, particularly if created in high volumes for mass production.
Quality: whether manufacturers are looking for strong, tensile or highly detailed components, the injection molding process is able to produce them at a high quality repeatedly.
This cost-effectiveness, efficient production time and component quality are just some of the reasons why many industries choose to use injection molded parts for their products.
Plastic injection molding is a versatile process that can be customized to meet different manufacturing needs. Depending on the complexity, materials, and end-use of the product, different injection molding techniques are used. Here are some of the most common types:
Custom Injection Molding
This is the most common type of injection molding, where a manufacturer creates plastic parts based on specific designs and requirements. It is widely used in industries like automotive, healthcare, and consumer goods to produce parts with precise dimensions and functionality.
Overmolding
Overmolding is a technique where multiple materials are molded together to create a single part. It is often used to add a soft-touch grip to tools, improve durability, or enhance aesthetics. For example, toothbrushes and power tool handles often have rubberized grips made using overmolding.
Insert Molding
In insert molding, a non-plastic component, such as a metal insert, electronic chip, or threaded fastener, is placed inside the mold before the plastic is injected around it. This technique is used in industries like electronics and automotive manufacturing to create strong, integrated parts.
Micro Injection Molding
This method is used to produce extremely small, high-precision plastic components—often less than a few millimeters in size. It is ideal for industries like medical devices, aerospace, and microelectronics, where precision is critical.
Gas-Assisted Injection Molding
In this process, pressurized gas (usually nitrogen) is injected into the mold along with the plastic, creating hollow sections within the part. This reduces weight, material usage, and production costs while maintaining strength. It is commonly used for automotive panels, furniture, and large plastic enclosures.
Thin-Wall Injection Molding
This technique is designed to produce lightweight and high-strength parts with extremely thin walls. It is widely used in packaging, electronics, and consumer goods to reduce material costs while maintaining product durability.
Each of these techniques serves a specific purpose, helping manufacturers create plastic parts that meet unique functional and aesthetic requirements.
In today’s world, plastics play an integral role in countless products we use daily, from packaging and toys to automotive components and medical devices. Custom plastic parts are specialized pieces designed to meet specific requirements for unique applications. These parts are essential in various industries, allowing for tailored solutions that enhance functionality, improve efficiency, and often reduce costs.
Whether you’re designing a prototype for a new gadget, manufacturing components for machinery, or creating packaging that stands out on store shelves, custom plastic parts provide the flexibility and adaptability needed to bring innovative ideas to life.
What is Injection Molding?
Injection molding is a manufacturing process in which molten material is injected into an already prepared mold and left to cool. Upon cooling, the material solidifies and takes the shape of the mold, before being ejected. While this process may be used for one-off productions, it is usually used in the mass production of identical parts. Materials most commonly used in injection molding are plastics or elastomers.
Due to its high output rate and consistency of quality, injection molding is widely used across different industries to create parts such as electrical components, automotive parts, basic consumer plastics, furniture parts, and many others.
Injection molding is the most widely used form of plastics processing worldwide. The process involves the injection of heated, liquefied plastic into a temperature-controlled mold under high pressure.
After the plastic fills the mold, it cools and solidifies into finished part(s) which can be easily removed when the machine opens up the mold. Each production sequence, from the closing of the mold to the injection “shot” to opening and removal of the part, is a “cycle.”
Injection molding processing is done in specialized injection molding machines, or IMMs, which are sized according to tons of mold clamping force. These may range from “micro” IMMs of just a few tons that produce extremely small parts in small molds to very large IMMs exceeding 3,000 tons of clamping force that can hold very large molds and make extremely large parts, such as automobile front fascia or bumper covers.
There are a number of considerations to bear in mind before undertaking injection moulding:
1. Financial
The entry cost for injection moulding manufacture can be high – given the cost of the machinery and the moulds themselves.
2. Production Quantity
It is important to determine how many parts you wish to manufacture so as to decide whether injection moulding is the most cost-effective production method.
3. Design Factors
Minimising the number of parts and simplifying the geometry of your items will make injection moulding easier. In addition, the design of the mould tool is important to prevent defects during production.
4. Production Considerations
Minimising the cycle time will aid production as will using machines with hot runner moulds and well thought-out tooling. Such small changes and use of hot runner systems can equal production savings for your parts. There will also be cost savings from minimising assembly requirements, especially if you are producing many thousands of even millions of parts.