
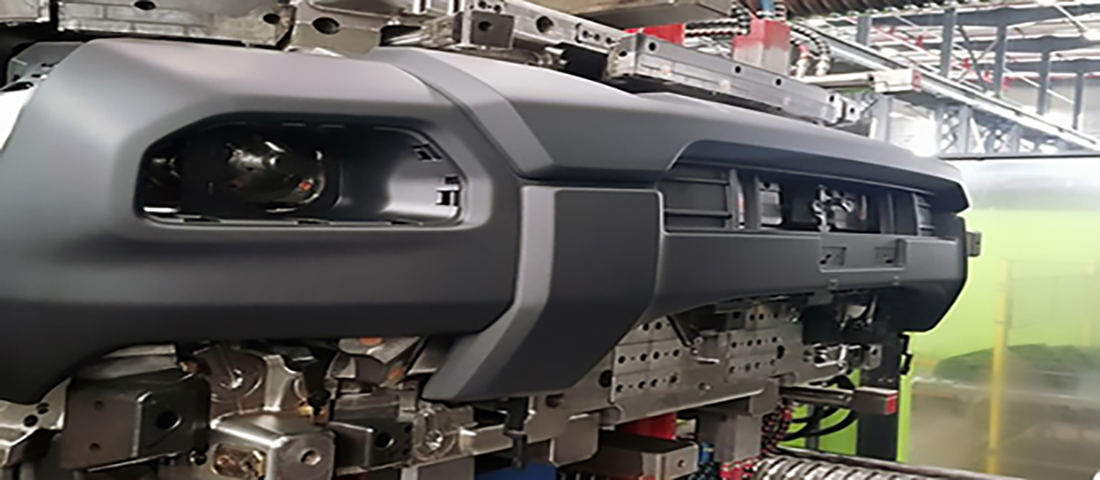
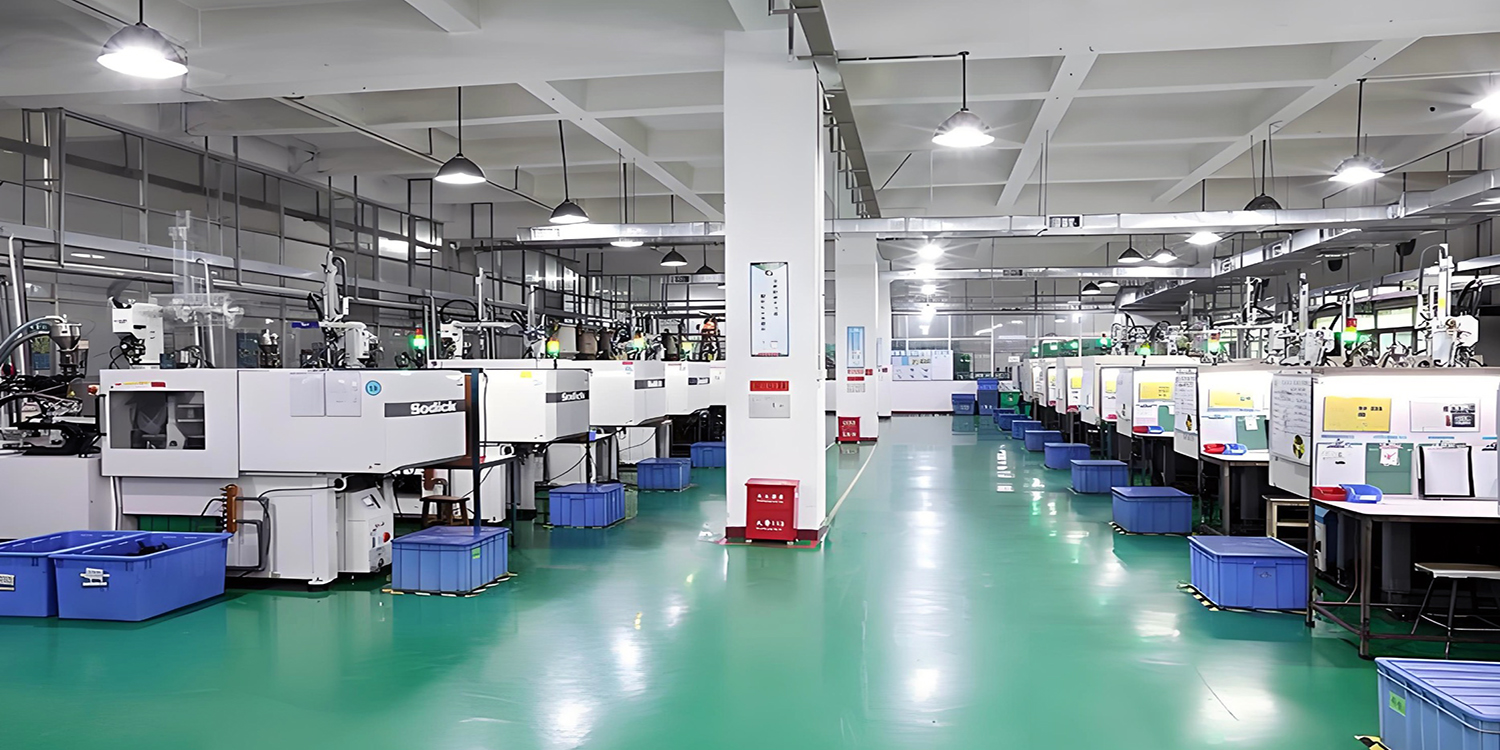
injection molding shop
FMS Molding Team Is Your Trusted Partner for Precision Mold & Injection Molding Since 2009
For nearly two decades, FMS has delivered world-class tooling and turnkey injection molding solutions to a global clientele. We specialize in custom plastic injection molding across highly demanding industries, including Medical, Automotive, Electronics, Packaging, Food & Beverage, and Outdoor Sports/Hunting.
Why Global Brands Choose FMS:
• Advanced Automation & Speed: 100% of our injection molding machines are integrated with high-speed robotics, ensuring consistent high quality, flawless precision, and minimized cycle times.
• High-Capacity 24/5 Operations: Operating on a 3-shift, 5-day schedule (with scalable weekend overtime), our workshop ensures your mass production deadlines are always met, no matter the volume.
• Engineering Excellence: Our veteran mold and design engineers bring deep cross-industry expertise, helping you optimize complex geometries for manufacturability (DFM) and cost efficiency.
• End-to-End Control: From initial tool design and steel/aluminum mold machining to final parts production, every step is managed entirely in-house by the FMS team for strict quality assurance.
Partner with FMS today to transform your complex designs into high-quality, cost-effective realities.
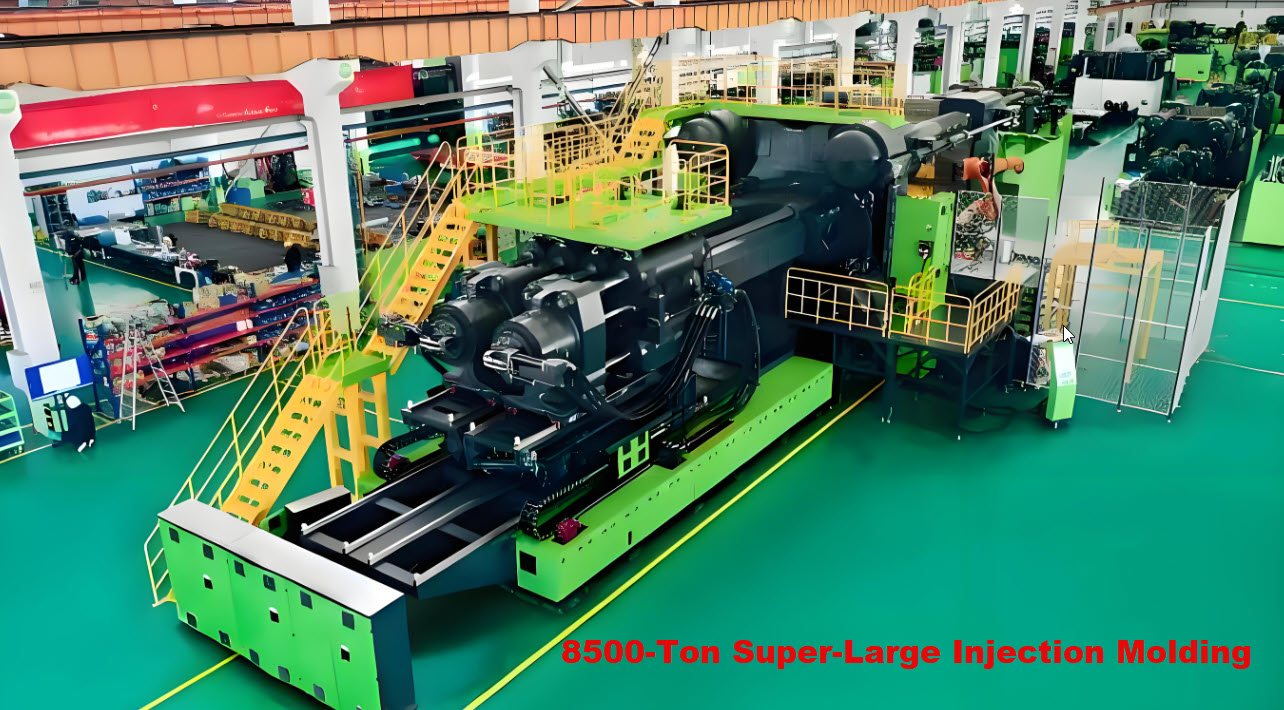
8500-Ton Super-Large Injection Molding Machine
How Does Injection Molding Work?
A special-purpose injection molding machine carries out injection molding. The manufacturing process is divided into the various steps listed below:
Step 1 – Creation of the Mold
The first step in injection molding is mold creation. The mold for the part to be manufactured is designed according to the specifications of the part’s 3D model, using computer-aided design, following several injection molding guidelines. It is then manufactured in two parts, usually using CNC machining. Molds are made from metals (mainly steel or aluminium).
Step 2 – Injection
The separate halves of the mold are placed in and held together tightly by the clamping unit of the injection molding machine. In the form of granules or pellets, the raw material is introduced into a barrel where it is heated at a high temperature and pressure till it melts. Now in molten form, the material is immediately injected into the mold cavity, filling the entire space in the mold. It then cools down and solidifies, forming the shape of the mold.
Step 3 – Ejection and Finishing
After the material has completely cooled and solidified, the mold is opened by the clamping unit and the solidified finished part is ejected. The finished part is subjected to some post-processing operations. These operations include removing excessive material and support structure, surface finishing, and, if required, painting, electroplating, heat treatment, etc.
Other Injection Molding Processes:
Over Molding
Over molding is an injection molding process that allows a part to be created from two different materials. The first material is molded and, before cooling down, the overmolding material is introduced, creating strong bonds between the substrate and the overmolding material. This technique is used to create multi-material objects with improved aesthetics and functionality, while eliminating the need for secondary operations.
Insert Molding
Insert molding is similar to over molding. In this injection molding technique a preformed object is inserted into the mold before the molten material is poured. With the point being to have the preformed material inserted into the molded object. An application of insert molding is inserting metal screw holes into plastic parts.
Metal Injection Molding
In this process, finely powdered metal is combined with wax, polypropylene binders, or other polymers to form a feedstock mix. It is then injected into the mold and left to cool. Once it solidifies, a portion of the blinder is removed using methods such as the catalytic process and the use of solvents.
Die Casting
The die casting process, also known as high-pressure die casting, is the forcing of molten metal under high pressure into a mold cavity. The process is as follows:
First is the preparation of the dies (molds), which entails the lubricating of the mold cavity to facilitate the easy removal of the casting and to control the temperature.
After that, the cast is closed and injected with molten metals under relatively high pressure between 1500 psi and 25400 psi.
Die casting products are made from nonferrous metals such as copper, zinc, aluminium, and lead.
Thin-wall Injection
This injection molding process is used to create plastic parts with very thin walls such as food packaging, parts of equipment, and lab apparatus. The sizes of these parts are larger than their thickness. This process of creating thin walls is more difficult than other processes.
Micro Injection Molding
Just as the name implies, “micro injection molding” is a molding process used to produce tiny plastic parts with weights of about 1 to 0.1 grams. This facilitates the manufacture of micro parts of various complicated geometries with maximum precision and accuracy.
Gas-assisted Injection Molding
In the production of thick plastic parts with injection molding, there’s the risk of distorted parts caused during the cooling process of the molten plastic. This is prevented from happening in gas-assisted injection. As the molten plastics solidifies, gas is introduced into the mold by gas channels, producing smooth surfaces.
The Future of Plastic Injection Molding
The future is bright for the plastic injection molding industry, with several new technologies showing a great degree of promise.
Internet of Things (IoT) technologies like sensors and automation solutions, for instance, allow for increased connectivity across the entire production system. This provides better visibility into the status of the injection molding process while also better positioning manufacturers to produce higher-quality parts at reduced costs. Automated solutions like robotic unloaders that can stack and unstack parts more efficiently can use programmable setups, sensors, and other IoT features to help shorten production timelines without sacrificing part quality.
Micro-injection molding is another emerging process that applies the mechanisms of injection molding at a microscopic scale. This is especially of interest in medical device manufacturing circles, where the technology could allow product teams to design smaller device assemblies capable of performing potentially life-saving procedures using less-invasive methods and tools.
Eco-friendly injection molding materials are increasingly in demand. While most thermoplastics can be reclaimed and reused simply by melting and re-integrating them, sustainability advocates are pushing for more ambitious goals. Out-of-the-box thinking is leading manufacturers to develop and use materials with less or no thermoplastic content, including next-generation, plant-based materials like corn- and flax-based plastics.
The Development and Emergence of Plastic Manufacturing. The history of plastic injection molding begins in 1868 when inventor John W. Hyatt patented the process of creating celluloid, a material originally intended to replace the ivory used in billiard balls. In 1872, Hyatt and his brother Isaiah patented the first injection molding machine, which used a simple plunger mechanism to push celluloid through a heated cylinder and into a mold. The device led to the development of a booming manufacturing industry that produced buttons, combs, collar stays, and other items from celluloid.
Soluble forms of cellulose acetate became available in the early 1900s, offering a much less flammable substitute for previous materials. In the lead-up to World War II, many of the thermoplastics commonly used today — including polystyrene and polyvinyl chloride (PVC) — were developed.
The Impact of World War II on Plastics Manufacturing
Developments in warfare technology, including aircraft, marine battleships, tanks, and other forms of weaponry, consumed vast amounts of raw materials during the course of the Second World War. The post-war industrial boom experienced by many developed Western countries coincided with skyrocketing demand for affordable materials that could be used to mass-produce parts. This was due in large part to how the war disrupted global shipping lanes and required the extraction of huge amounts of natural resources to manufacture tanks, ships, and other war-time products, leading to worldwide shortages of rubber and metal.
Thermoplastics presented affordable options capable of filling many of the market gaps created by these material shortages. Injection molding made it possible for manufacturers to quickly and cost-effectively manufacture parts in large volumes. As markets and supply chains worldwide shifted toward plastic, injection molding emerged as a mainstay and fixture for modern manufacturing companies.
In 1946, James Watson Hendry’s extrusion screw injection machine revolutionized the modern plastic injection molding field. The machine’s rotating screw gave the operator better control over the production process, resulting in significant improvements to the quality of the injection-molded parts. Hendry also pioneered the gas-assisted injection molding process, which made it possible to manufacture long and complex hollow parts.
During the latter half of the twentieth century, plastic materials became more advanced and competitive, offering comparable strength to some metals but at a greatly reduced weight.
Plastic production overtook steel production in terms of market share by the 1970s, and the introduction of lightweight aluminum molds in the 1990s offered a faster, more cost-effective substitute to steel tooling in some instances.
Injection molding is done in a 6-step process.
1) The first step of injection molding is the process of clamping. The clamping unit is what pieces together the mold before the injection takes place. The two sides of the mold are placed into the unit and then the machine pushes the two halves together to prepare for the next step: injection.
2) Once the clamping phase is complete and the two halves are put together, the injection of the plastic begins. The plastic, usually in the form of pellets, are then pumped into a container in which they are melted down to a complete liquid. This liquid is then injected into the mold, maintaining temperature throughout the process.
3) Next comes the dwelling phase, in which the plastic is filled to the entirety of the mold. This is done through pressure. Pressure is applied to the mold so that way the plastic covers all of the mold cavities to ensure the product will come out correct.
4) The fourth step is the cooling stage and is the most straightforward. The mold is left alone so the plastic inside can cool and start to form as a solid inside of the mold.
5)Next step is the mold opening.
6) This is followed by the final step of ejection, which reveals the final plastic product from the mold.
Injection molding has become one of the most popular manufacturing processes used in the world today. It offers numerous benefits, which we will now look at below:
Fast production speeds
One of the main benefits of injection moulding is that even complex products can be produced at rapid speeds. The process is also largely automated and requires little human interaction.
Low manufacturing costs
Thanks to the automated nature of injection molding, manufacturing costs are kept low. This makes it especially ideal for use in producing products where low manufacturing costs are important to compete in the market.
Low levels of waste
Injection molding produces very low levels of waste, whilst any plastic waste that is produced can usually be recycled. This makes injection moulding an extremely environmentally friendly process and therefore a good choice for any organisation looking to limit their impact on the world.
High strength
Don’t think that the high-speeds and low-costs of manufacture have a negative impact on the end product. Fillers can be added during the molding process to enhance the strength and durability of the product as required.
High levels of flexibility
Another beauty of injection molding is that the process is extremely flexible. Different materials can be easily injected into the mold to produce different variations – and with co-injection, it’s even possible to simultaneously inject different materials.
Injection molding Advantages
The main advantage of injection moulding is being able to scale up production to produce a large number of parts. Once the initial costs of the design and the moulds have been covered, the price of manufacturing is very low. The cost of production drops as more parts are produced.
Injection moulding also produces minimal wastage when compared to traditional manufacturing processes like CNC machining, which cuts away excess materials. Despite this, injection moulding does produce some waste, mainly from the sprue, the runners, the gate locations, and any overflow material that leaks out of the part cavity (also called ‘flash’).
The final advantage of injection moulding is that it allows for the production of many identical parts, which allows for part reliability and consistency in high volume production.
Injection molding Disadvantages
While injection moulding has its advantages, there are also a number of disadvantages with the process.
Up-front costs can be high for injection moulding, particularly with regard to tooling. Before you can produce any parts, a prototype part needs to be created. Once this has been completed, a prototype mould tool needs to be created and tested. This all takes time and money to complete and can be a costly process.
Injection moulding is also not ideal for producing large parts as a single piece. This is because of the size limitations of injection mould machines and the mould tools. Items that are too large for an injection moulding machine’s capability need to be created as multiple parts and joined together later.
The final disadvantage is that large undercuts require experienced design to avoid and can add even more expense to your project.
these are some tips for choosing an injection molding Service provider:
Is the new molding house educated on your company’s needs? Are they updated on the processing manuals supplied by the material manufacturer? Your molding company should be aware of the mechanical properties that were advertised and defined in the literature provided by the material manufacturer. Your engineering department believed these mechanical properties to be important, therefore they should be known and implemented. They will ultimately result in the survival of your product in its finished environment.
you also need to konw if your new molder have the proper knowledge to process the resin of my choice? Do they know how to utilize the best molding practices? Are they aware of resin drying time, heat history, and molding temperatures, etc., etc.? Be sure your new molder is aware of your machine settings. This is crucial in determining a dependable and high quality outcome for your products.
Please check carefully if the prospective molder have an effective training program for the employees. if the employees aware of expectations, processes, and deadlines; Communicate your needs with your potential partner. whether the new molding house know how to handle raw materials; specifically the materials that will develop new products, Knowledge of the materials is essential in the molding technique.
you should know you can trust your molding house to properly do the job, you have an honest and reliable relationship with your new partner. Good communication with your new molder is imperative to satisfying results. Continuous interaction with your new partner and creating a solid foundation of your business relationship will only benefit the development process.
cost is the important aspect of your project. Quality stands the test of time; it may not be obvious until parts fail to do their job in the finished product. You supply your customers with reliable products. Be sure your molding company is supplying you with a dependable process.
Once the injection molds have been designed to the customer’s specifications and the presses pre-programmed, the actual molding process is very quick compared to other methods of molding. Plastic injection molding process hardly takes times and this allows more parts to be manufactured from a single mold. The high production output rate makes plastic injection molding more cost effective and efficient. Typically, hot-runner ejection mold systems produce parts with more consistent quality and do so with faster cycle times, but it’s not as easy to change colors nor can hot runners accommodate some heat-sensitive polymers.
Plastic injection molding is an automated process. A majority of the injection molding process is performed by machines and robotics which a sole operator can control and manage. Automation helps to reduce manufacturing costs, as the overheads are significantly reduced. Furthermore, with reduced labor force the overall cost of manufacturing the parts is reduced and this cost saving can easily be passed on to the customer.
Furthermore, automation allows for making precise and accurate injection molds. Computer aided design (CAD) and computer aided manufacturing (CAM) allow close tolerances during the making of the molds.