The Importance Of Product Design
Product design is the cornerstone of successful manufacturing. In fact, product molds represent nearly 40% of the entire molding industry, underscoring just how critical the design phase is to a product’s ultimate success. However, bringing a concept to life requires adherence to strict engineering rules and highly specialized expertise. It demands professionals.
Backed by decades of manufacturing excellence, the FMS Design Team transforms your concepts into market-ready realities. We don’t just design; we optimize your products for scalability, cost-efficiency, and premium quality.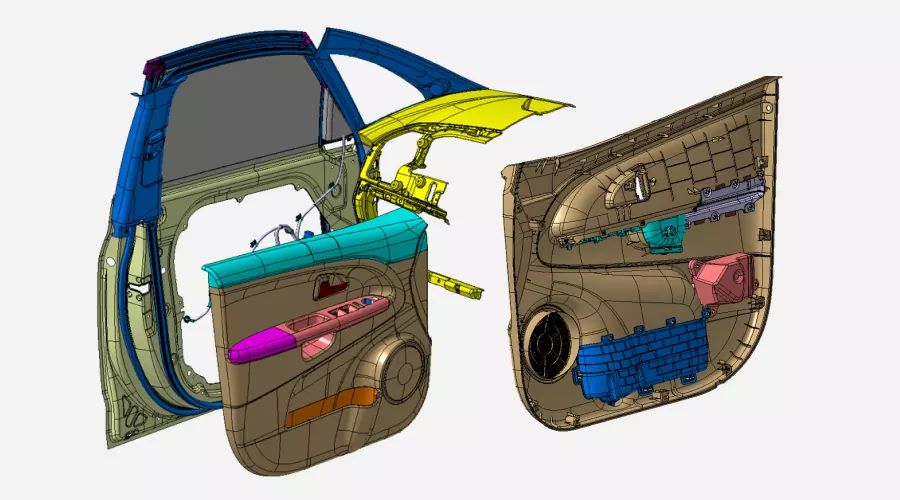
Seamless Collaborative Design
We have broken down geographic barriers with our advanced Internet-enabled Collaborative Design system. Distance is no longer a factor. You can review designs, analyze structures, and assemble virtual prototypes alongside our engineers in real time.  It feels exactly like having an in-house design department right next door—a seamless partnership that consistently earns the highest satisfaction ratings from our global clients.
Why Choose FMS for Product Design?
At FMS, we bridge the gap between innovative concept and flawless production. Here is how our unique design advantages accelerate your success:
• Design Built for Manufacturing (DFM): Backed by extensive expertise in molding simulation analysis and advanced mold design, our team ensures your products are optimized for production from day one—minimizing errors and reducing time-to-market.
• Strategic Global Hub Advantage: Located at the absolute epicenter of the world’s mold-making and molding industry, we have direct access to cutting-edge techniques and top-tier manufacturers. This keeps our designs at the forefront of global innovation.
• Premium Quality, Competitive Edge: We deliver professional, efficient, and high-integrity design services that meet strict Western quality standards—offering you premium engineering expertise at a highly competitive price point.
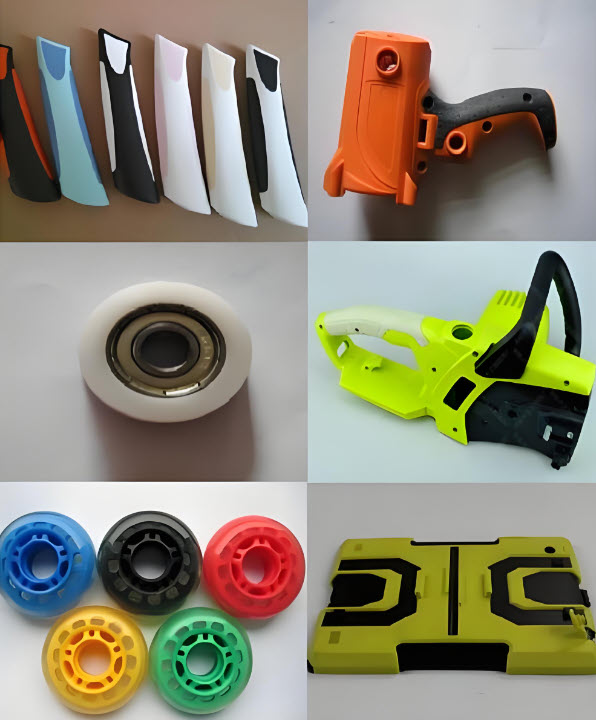
Elevate Your Product with High-Impact Design
Great design shouldn’t cost more. We transform standard product concepts into eye-catching, market-ready products that consumers actually want to buy—without driving up production costs.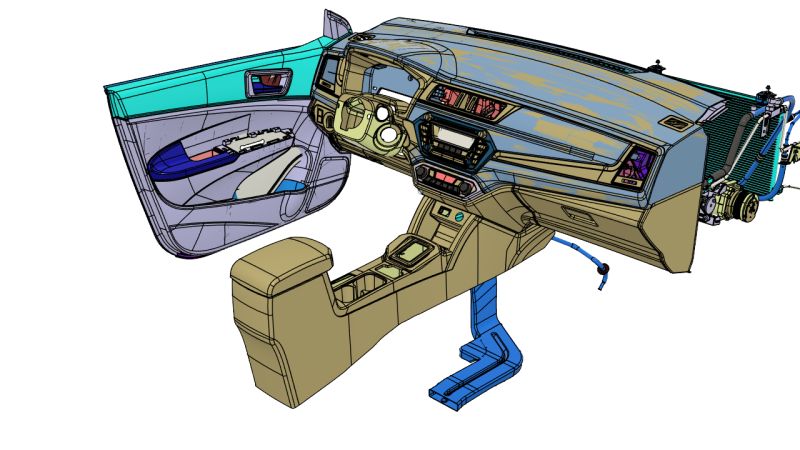
Utilizing industry-leading CAD systems, our team combines advanced surface modeling expertise with a deep understanding of economical injection molding. But we provide more than just technical tools. We bring the artistic vision and stylistic intuition needed to give your product a competitive edge. Let us help you turn your next big idea into a beautifully engineered, commercial success.
Maximizing Performance Through Design for Manufacturing (DFM)
Designing parts with advanced materials requires a unique mindset: they must be strictly engineered for seamless production. While basic product design is common, achieving true excellence demands deep expertise in manufacturing processes and tooling functionality.
With a proven track record in world-class mold design, we possess an unmatched understanding of tooling and molding dynamics. By combining this hands-on manufacturing insight with our advanced CAD and FEA stress analysis capabilities, we deliver optimized, production-ready designs that elevate your product’s performance from day one.
Why Stress Analysis is Critical for Plastic Design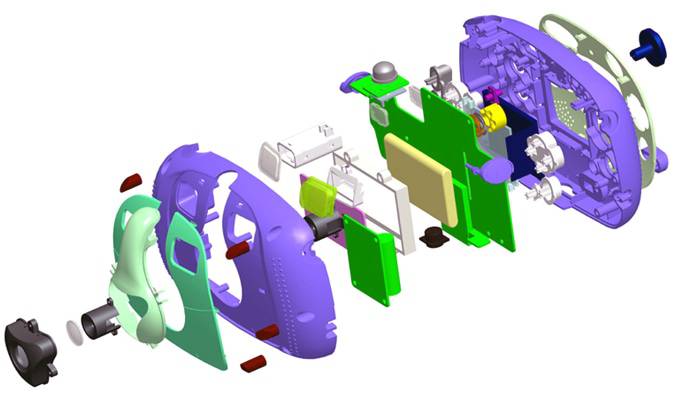
 It is well established that the structural characteristics of plastics differ fundamentally from those of metals. However, even a foundational concept like “stress” takes on a completely different meaning when applied to a plastic component versus a metal one. The core challenge for engineers is understanding exactly how these divergent material properties impact the design process.
While plastics are often perceived as a low-cost material, they are actually quite expensive from a unit-volume or load-bearing perspective. Their true cost-efficiency stems from the high-speed injection molding process. Given this reality, a 100% plastic design isn’t always the most cost-effective solution.
Furthermore, while plastics excel at handling intermittent loads, they are prone to permanent deformation (creep) even under low, long-term stress. In many designs, simply adding more plastic is not a viable fix. Instead, strategically integrating a small amount of load-bearing metal components into a primary plastic structure often yields a significantly superior, high-performance product.
Working with you to develop and design your plastic injection molded component. To ensure a quality part, there are three major areas of focus throughout the design stage:
Proper plastic part design
Proper material selection plastic part design
Processing conditions for plastic injection molding
Designing Parts for Up & Down Molding Helps Control Cost
Designing a part that can be molded with a “straight pull” or “up & down” motion is a great way to keep the cost of the mold down. A straight pull mold is designed so that when the two halves (A side and B side) of the mold separate from each other, there is no plastic blocking the path of the metal in the direction of the pull. Undercuts on the part cause this blockage of path and require an action in the mold (cams, core pulls, etc.). Action in the mold can have a major impact on the cost (and overall size) of a mold.
Uniform Wall Thickness Helps to Prevent Defects
Proper wall thickness is one of the most fundamental requirements in designing a part for plastic injection molding. Plastic shrinks as it cools which can lead to defects such as sink marks, voids, stresses, and warping. Plastic resin solidifies in the mold nearer to the outside of the part (closest to the mold surface). Thick sections of a part tend to pull inward, creating stresses, sink marks, or voids. Since thinner sections cool quicker, stress can build in the part between thinner and thicker sections, resulting in part warpage.
Draft Allows for Parts to Release from the Mold
Draft is required on all parts in the direction of mold movement in order to allow parts to release or eject from the mold properly. Draft is the angle in which the part is tapered to allow it to release. As the part cools, it tends to want to shrink to the core side of the mold. Adding draft helps the part to release. Most parts or applications require a minimum of 1/2 to 1 degree, however 11/2 to 2 degrees is widely accepted as the norm.
Understanding of Plastic Product Design and Development?
Plastic Product design and development related to designing new products from plastics. They are a modern process that involves the following steps: Concept, design, and production. This involves aspects such as the choice of materials, adherence to design theories, and manufacturing requirements in coming up with products that suit a certain user need or market demand.
Different Types of Processes Used in Plastic Product Design and Development
Here are some of the common types of processes we can use for plastic product design and development;
1. Injection Molding
This method of molding plastics is one of the most frequently used technologies for creating parts for mass production. It is a process by which a desired shape is created by pouring a heated liquid material which is plastic in this case under a high-pressure chamber and appears in the plastic injection mold in a desired shape already created. In another case when the plastic remains hot, the mold opens and releases the part but the final shape remains that which is intended. It is a highly efficient technique for volume production because the process is fast, and parts can be produced with close tolerances and very little material being used up.
2. Blow Molding
Blow molding is particularly applied for the manufacturing of hollow products made of plastic materials such as bottles and containers. The first step involves softening the plastic using heat and then pouring it on a mold. Air is then forced into the mold, and the molten plastic is forced into the hollow shape of the inner surface of the mold. When it comes to the idea that blow molding is good for products that have to be lightweight, resistant to impact, and should have the ability to contain a liquid.
3. Thermoforming
It is mainly comprised of heating a plastic sheet and transforming it into a flexible form of plastic. The material is then draped over the mold and via a vacuum-forming process is drawn over the surface of the mold and leaves when the material cools. Thermoforming is more widely applied in the packaging industry, disposable trays, and containers. So, this method is characterized by relatively low costs and allows the creation of thin light products in large quantities.
4. Rotational Molding
Rotational molding or roto-molding is a slower method of molding that is more appropriate for producing large empty articles such as tanks, playing equipment, and boats such as kayaks. Here, powdered plastic is put into a mold that is then heated and is also compounded on a two-plane system. As the mold rotates the powder melts and the bonding of the powder to the interior walls of a mold is done providing a strong product without seams. It is suitable for the generation of an extensive and rather thin-walled container including varying wall thickness.
5. 3D Printing
3D printing or Additive manufacturing process involves the construction of an object using a physical model created from a computer source. While most other technologies are removal- or casting-based, 3D printing enables direct control of intricate surface geometries and voids. Because it can make a physical model of the design without the use of the costly mold, it is frequently used for prototyping. It is also appropriate to use if a production run is small or on assemblies that require specific materials.
Designing a plastic part for manufacturability involves many important factors that touch on all areas of part design, tooling, material selection and production. First, it is essential to build parts around functional needs by keeping design intent or the end use in mind. Consider weight reductions, the elimination of fabrication and assembly steps, improving structural components, reducing costs and getting products to market quicker. Here are 8 important factors to consider to meet your plastic part design goals for a successful production process.
1. Material Considerations
Manufacturers often select a familiar grade of plastic from a similar application or rely on recommendations from suppliers. Resins chosen this way may be adequate, but are rarely optimal. Plastic selection is a complex task that involves many considerations, such as:
Temperature: Thermal stress that may occur during normal and extreme use conditions, as well as during assembly, finishing and shipping.
Chemical resistance: The effects that occur when any solid, liquid or gas come in contact with the part.
Agency approvals: Governmental and private standards for properties such as heat resistance, flammability, and electrical and mechanical capabilities.
Assembly: The plastic’s cooperation with all assembly steps like bonding, mechanical fasteners and welding.
Finish: The material’s ability to produce the desired finish such as gloss, smoothness and other appearance values as it comes from the mold.
Cost: Resin pricing as well as the cost calculations for manufacturing, maintenance, assembly and disassembly to reduce labor, tooling, finishing and other costs.
Availability: The resin’s availability in regard to amount needed for production.
2. Radius
Radius should always be a consideration in regard to the part’s thickness – eliminating the likelihood of areas of high stress and possible breakage of the part. A general rule of thumb is that the thickness at a corner should be in the range of 0.9 times the nominal thickness to 1.2 the nominal thickness of the part.
3. Wall Thickness
Designing your part so that wall thickness is consistent can help avoid many part defects that can occur during the manufacturing process. When plastic melts, it flows to the areas of leas resistance. If your part has inconsistent thicknesses throughout, the melt may flow into the thick areas first (depending on gate locations). When this occurs, the thin areas may not fill properly. Additionally, thicker areas tend to cool more slowly and are at risk for voids or sinking defects. Designing your part with rounded corners will also aid in the proper filling of the part during the molding process.
4. Gate Location
Gates are critical to ensuring the resin flows properly into the mold. These small components of your design are what directs the flow of resin from the runners to then be distributed through the part. Type of gate and placement has an important impact on the part’s overall quality and viability.
5. Draft
Draft is the amount of taper on the vertical walls of the plastic part. Without draft, a part may not eject from the mold, or may sustain damage during ejection. Typically, draft angles between 1° and 2° are required, but can vary depending on part restrictions and specifications.
6. Inclusion of Ribs
A plastic part that has been designed with a minimal wall thickness will not be as strong as a thicker part – which is why the inclusion of ribs may be needed to help reinforce the part’s strength. Depending on the material used, rib thickness should be between 50 – 70 percent of the relative part thickness to avoid sink marks. To avoid sinking, designers may core out material to reduce defect risk.
7. Mold Shrinkage
The shrinkage that occurs during the plastic part molding process can be as much as 20 percent by volume. Crystalline and semi-crystalline materials are most prone to thermal shrinkage. Amorphous materials are known to shrink less. Here are a few easy ways to avoid molding shrinkage issues:
Adjust the formulation
Adjust the mold design to get the dimension you want based on the expected shrinkage that will occur
Optimize the processing parameter such as molding temperature, melt temperature, and injection speed/pressure/time, cooling time.
8. Special Features
Plastic parts should be designed so that mold tools open and eject the part easily. When a part is released, the two sides of an injection mold separate in the opposite direction. When special features like holes, undercuts or shoulders prevent the release from happening, it may be required that side actions be incorporated into the design.
Side actions pull coring in a direction other than the direction of the mold separation. This adds flexibility to the part design and at times, may increase the cost of the mold.
Working with an experienced plastic injection molder and engineering team is a critical component to avoiding many issues that can occur during the design and development process. If you keep these factors in mind during the design process, and align with a knowledgeable plastics engineer, you will be on track to get your product to market quicker and within your budget.
To ensure a plastic quality part, there are three major areas of focus throughout the design stage:
Proper plastic part design
Proper material selection plastic part design
Processing conditions for plastic injection molding
our designers and engineers have over 50 combined years of experience in designing parts for plastic injection molding, selecting materials, and processing resins (specializing in engineering and high performance resins). which was designed to demonstrate the basic elements of proper plastic part design.
Designing Parts for Up & Down Molding Helps Control Cost
Designing a part that can be molded with a “straight pull” or “up & down” motion is a great way to keep the cost of the mold down. A straight pull mold is designed so that when the two halves (A side and B side) of the mold separate from each other, there is no plastic blocking the path of the metal in the direction of the pull. Undercuts on the part cause this blockage of path and require an action in the mold (cams, core pulls, etc.). Action in the mold can have a major impact on the cost (and overall size) of a mold.
1) Uniform Wall Thickness Helps to Prevent Defects
2) Draft Allows for Parts to Release from the Mold
3) Holes Enhance Part Functionality and Reduce Weight
4) Bosses Aid in Assembly and Mounting
5) Ribs Enhance Part Strength and Stability
6) Adding a Radius Reduces Stress on Corners
Designing a plastic part for manufacturability involves many important factors that touch on all areas of part design, tooling, material selection and production. First, it is essential to build parts around functional needs by keeping design intent or the end use in mind. Consider weight reductions, the elimination of fabrication and assembly steps, improving structural components, reducing costs and getting products to market quicker. Here are 8 important factors to consider to meet your plastic part design goals for a successful production process.
1. Material Considerations
Manufacturers often select a familiar grade of plastic from a similar application or rely on recommendations from suppliers. Resins chosen this way may be adequate, but are rarely optimal. Plastic selection is a complex task that involves many considerations, such as:
Temperature: Thermal stress that may occur during normal and extreme use conditions, as well as during assembly, finishing and shipping.
Chemical resistance: The effects that occur when any solid, liquid or gas come in contact with the part.
Agency approvals: Governmental and private standards for properties such as heat resistance, flammability, and electrical and mechanical capabilities.
Assembly: The plastic’s cooperation with all assembly steps like bonding, mechanical fasteners and welding.
Finish: The material’s ability to produce the desired finish such as gloss, smoothness and other appearance values as it comes from the mold.
Cost: Resin pricing as well as the cost calculations for manufacturing, maintenance, assembly and disassembly to reduce labor, tooling, finishing and other costs.
Availability: The resin’s availability in regard to amount needed for production.
2. Radius
Radius should always be a consideration in regard to the part’s thickness – eliminating the likelihood of areas of high stress and possible breakage of the part. A general rule of thumb is that the thickness at a corner should be in the range of 0.9 times the nominal thickness to 1.2 the nominal thickness of the part.
3. Wall Thickness
Designing your part so that wall thickness is consistent can help avoid many part defects that can occur during the manufacturing process. When plastic melts, it flows to the areas of leas resistance. If your part has inconsistent thicknesses throughout, the melt may flow into the thick areas first (depending on gate locations). When this occurs, the thin areas may not fill properly. Additionally, thicker areas tend to cool more slowly and are at risk for voids or sinking defects. Designing your part with rounded corners will also aid in the proper filling of the part during the molding process.
4. Gate Location
Gates are critical to ensuring the resin flows properly into the mold. These small components of your design are what directs the flow of resin from the runners to then be distributed through the part. Type of gate and placement has an important impact on the part’s overall quality and viability.
5. Draft
Draft is the amount of taper on the vertical walls of the plastic part. Without draft, a part may not eject from the mold, or may sustain damage during ejection. Typically, draft angles between 1° and 2° are required, but can vary depending on part restrictions and specifications.
6. Inclusion of Ribs
A plastic part that has been designed with a minimal wall thickness will not be as strong as a thicker part – which is why the inclusion of ribs may be needed to help reinforce the part’s strength. Depending on the material used, rib thickness should be between 50 – 70 percent of the relative part thickness to avoid sink marks. To avoid sinking, designers may core out material to reduce defect risk.
7. Mold Shrinkage
The shrinkage that occurs during the plastic part molding process can be as much as 20 percent by volume. Crystalline and semi-crystalline materials are most prone to thermal shrinkage. Amorphous materials are known to shrink less. Here are a few easy ways to avoid molding shrinkage issues:
Adjust the formulation
Adjust the mold design to get the dimension you want based on the expected shrinkage that will occur
Optimize the processing parameter such as molding temperature, melt temperature, and injection speed/pressure/time, cooling time.
8. Special Features
Plastic parts should be designed so that mold tools open and eject the part easily. When a part is released, the two sides of an injection mold separate in the opposite direction. When special features like holes, undercuts or shoulders prevent the release from happening, it may be required that side actions be incorporated into the design.
Side actions pull coring in a direction other than the direction of the mold separation. This adds flexibility to the part design and at times, may increase the cost of the mold.
Most of the plastic product manufacturing organizations face multiple problems during manufacturing. Some common challenges faced by plastic manufacturing organizations are:
When a part is to be ejected against the draft direction – in such cases, the designer must be aware of manufacturing constraints and the quantum of force ejection that can be done.
When there are multiple no. of lifter or slider arrangements – in such cases, tool designer must analyse the slider movement with respect to time taking into consideration the cooling time. So, in those cases, CATIA Mould Tooling workbench can really be helpful.
When designer reverse engineers a product – in such cases, achieving the desired parameter in terms of performance is a challenging task. This can be mitigated by simulating the results through virtual analysis.
Assembly of rubber part and plastic part – for a leak proof product, the designer should not prefer the parting line as it creates material flushes in those particular junctions and it results in leakage as well as breakage or tear of rubber parts from inner surface. All these challenges can be addressed beforehand by analysing the parting line position and by doing a mock up.
Plastic part design consideration plays a significant role in designing and manufacturing a plastic component. Whenever a Product Designer designs a plastic part, it is important to take care of factors such as the moulding process, selection of material, mass manufacturing process and overall area of the part around the functional need by keeping the design intent intact or the end use in consideration.
Plastic parts manufacturing is a nuanced methodology that merges artistry with intricate mechanical engineering. This multifaceted industry extends from the manufacturing plants all the way to your local stores, providing countless objects we use daily. It refers to the production process involved in transforming plastic materials into a wide range of plastic parts, including different types of plastics.
The transformation happens in various ways, each tailored to produce high-quality goods with distinct characteristics and applications. Processes like injection molding, extrusion manufacturing process, fabrication, and CNC machining are some of the core techniques in plastic parts manufacturing. The production process involved in manufacturing complex parts made of thermosetting plastics is a careful blend of technology, material science, and craftsmanship.
A critical factor in the manufacturing process is the type of plastic material used. Thermoplastics such as polyethylene, polypropylene, and polystyrene are commonly used in the industry. Nylon is another thermoplastic that is widely used due to its high strength, durability, and resistance to abrasion. Additionally, polymers called thermosets are another type of plastic material that are used in manufacturing due to their ability to withstand high temperatures and resist deformation. Each plastic processing method also directly relates to the produced part’s complexity, mechanical properties, and cost-effective large quantities manufacturing.